Assembly Process
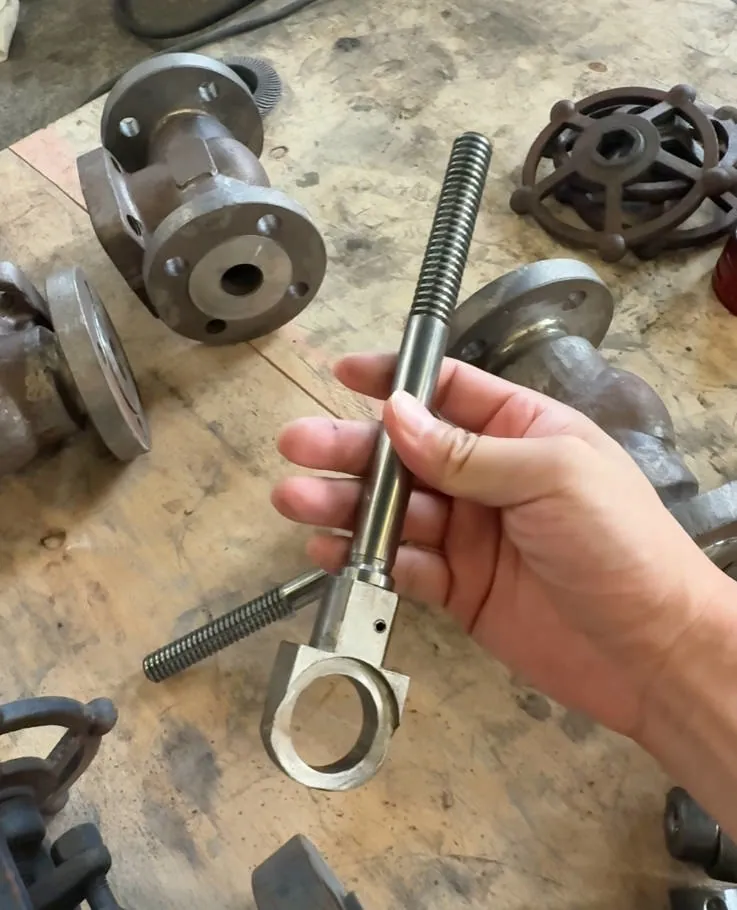 01
Stem-to-Gate ConnectionConnecting the stem securely to the slab gate.
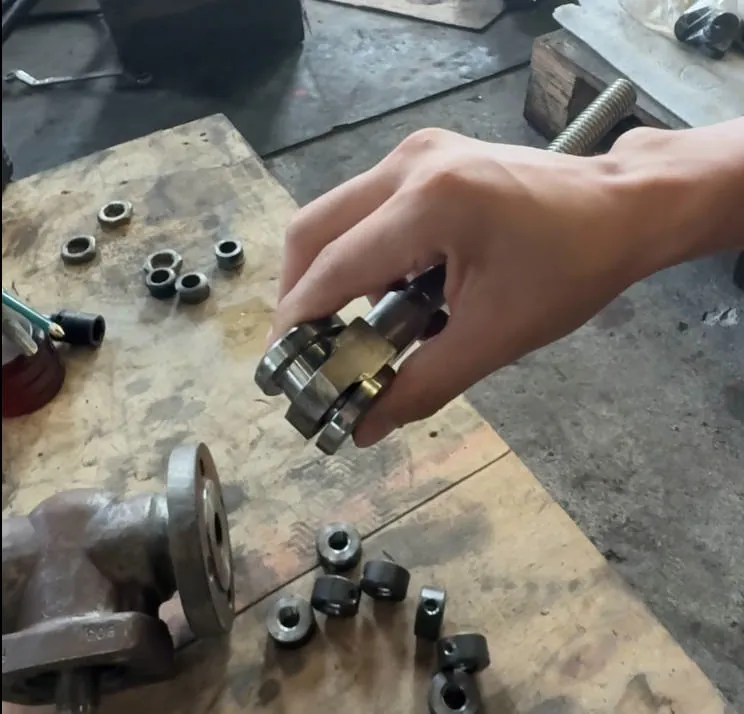 02
Seal Component PreparationChecking and preparing the internal sealing components.
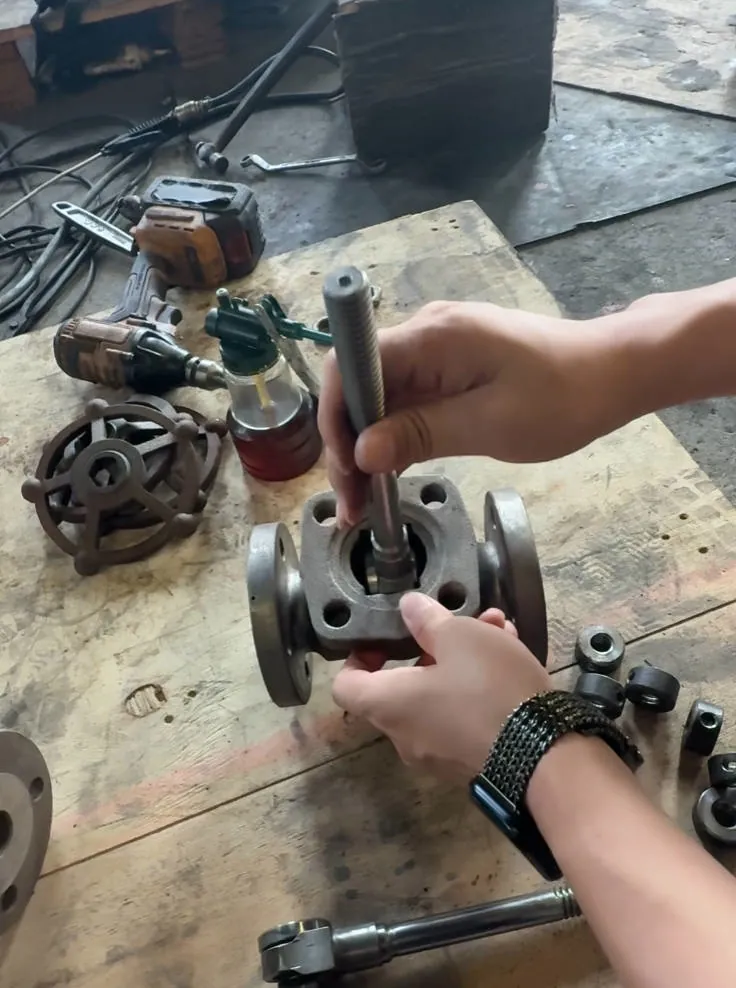 03
Internal Assembly PositioningInstalling the assembled internal parts into the valve body.
Assembly and Inspection Scope
This production update documents the assembly stage of a 2-inch Class 600 forged slab gate valve. The final configuration and acceptance criteria are governed by the approved drawing, purchase specification and inspection plan; photographs alone do not establish the valve's complete pressure-temperature or sealing capability.
Items confirmed during assembly
- Body, bonnet and trim identification against the production traveller and material records.
- Gate, seat and stem alignment, operating movement and accessible sealing surfaces.
- End connection, face-to-face and other specified dimensional checks.
- Packing, bolting, accessories, marking and preservation requirements.
Documents to request before shipment
Depending on the purchase order, the document package may include material certificates, dimensional records, applicable NDE reports, shell and seat pressure-test records, coating or preservation records, nameplate details and final packing photographs.
For a comparable valve, provide the service medium, design pressure and temperature, end connection, bore requirement, body and trim materials, sealing direction, operating method, quantity and required inspection scope.
Need a forged slab gate valve quotation?
Send the datasheet or line conditions for a project-specific technical review.
Request a QuoteProject release basis
Project release should reference the approved drawing, bill of materials, inspection and test plan, pressure-test procedure and traceability records. Dimensions, trim, seat-leakage acceptance, coating, NDE extent and shipping preservation remain order-specific until they are confirmed in the purchase order and approved manufacturing documents.