Manufacturing and Test Process
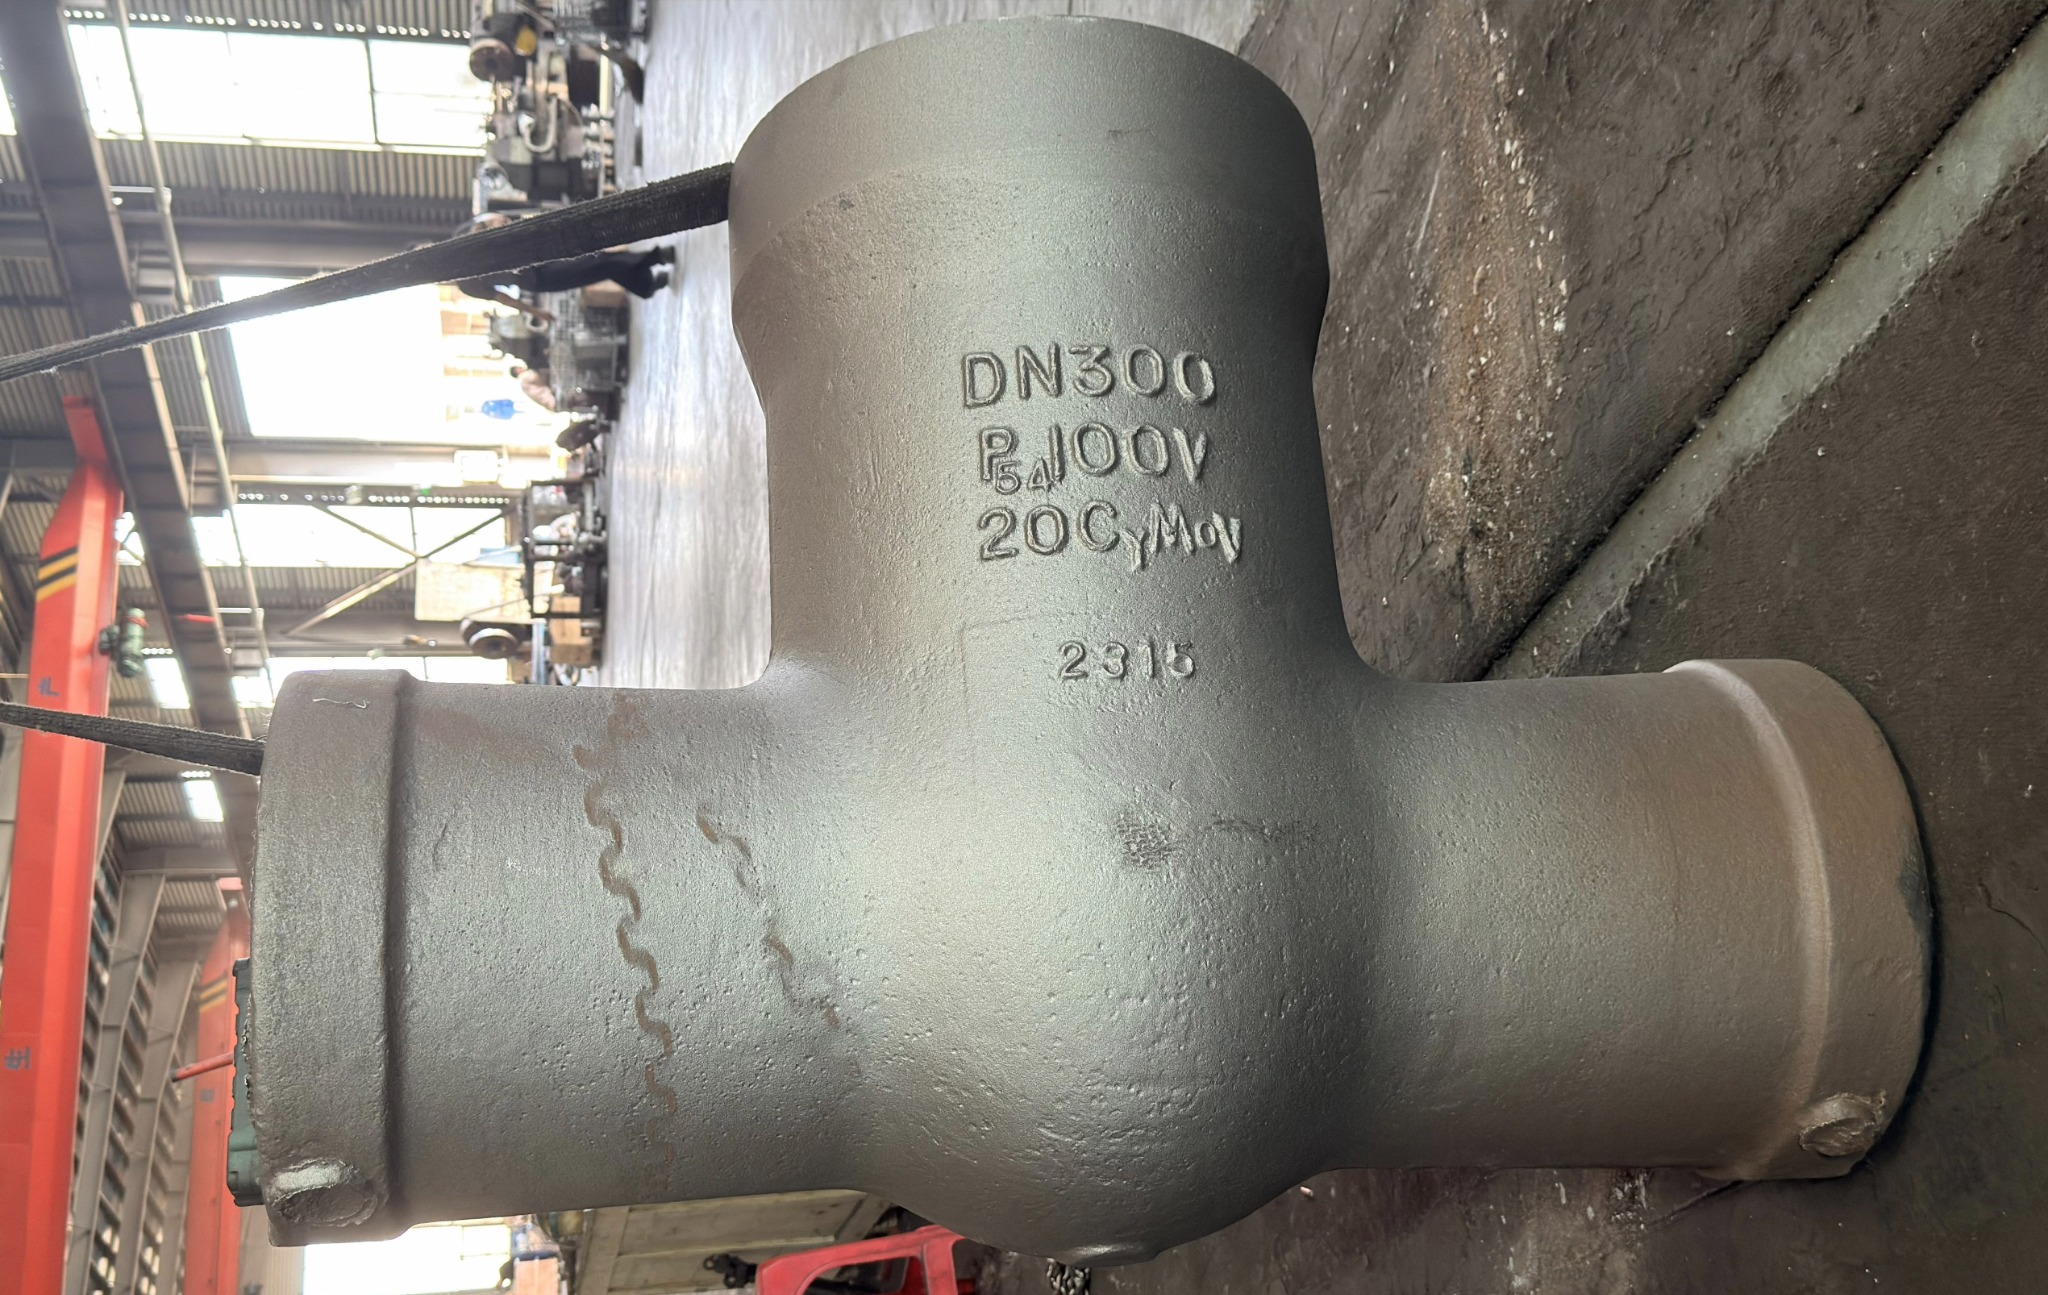 01
Valve Body IdentificationCast-in size and material markings remain visible for identification during production.
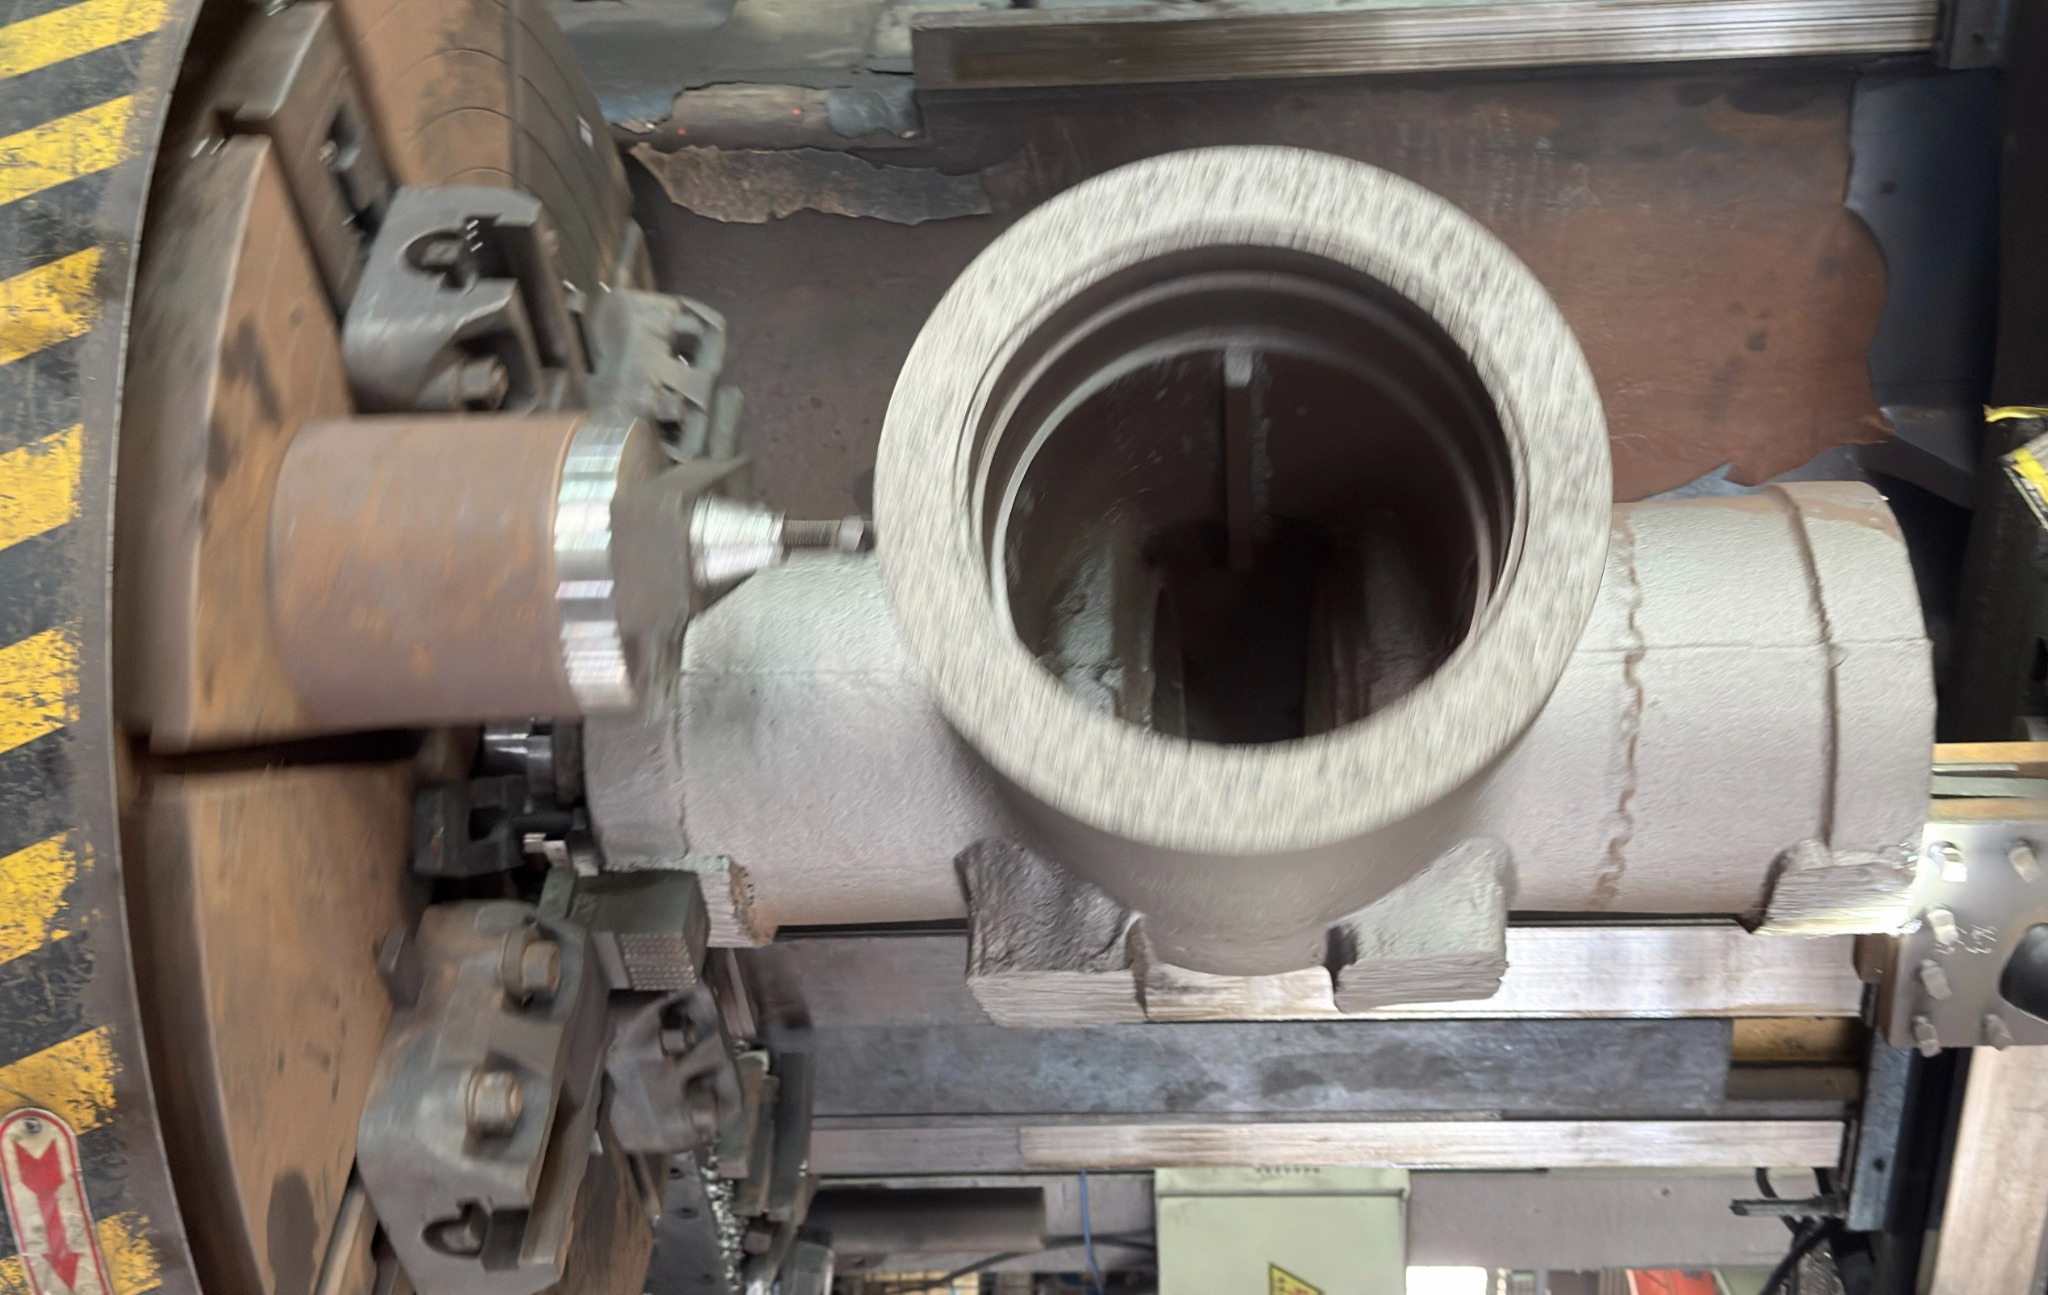 02
Valve Body MachiningThe valve body is secured on the machine tool for controlled interface machining.
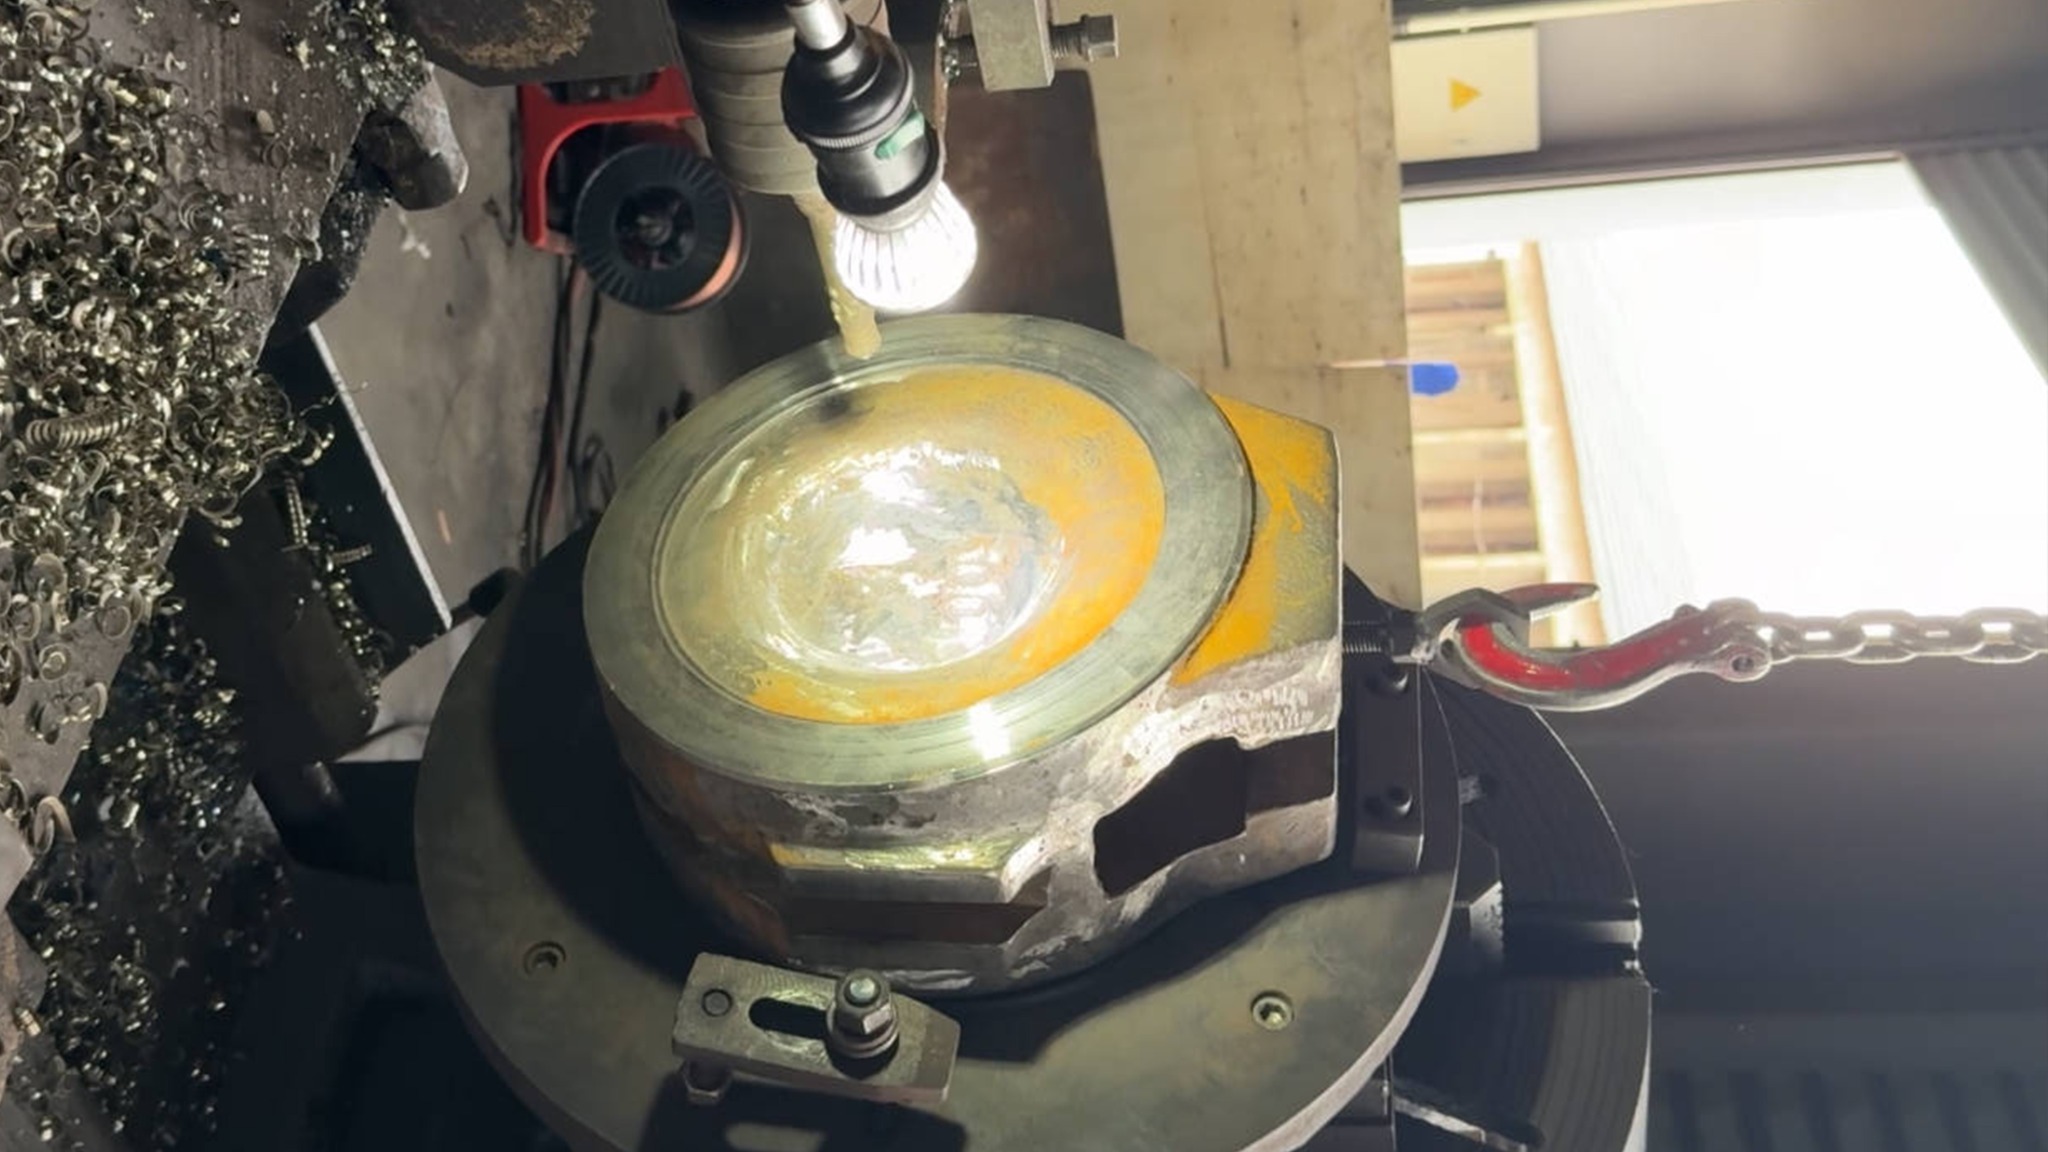 03
Gate Sealing Surface Precision MachiningPrecision machining and finishing of the gate sealing surfaces.
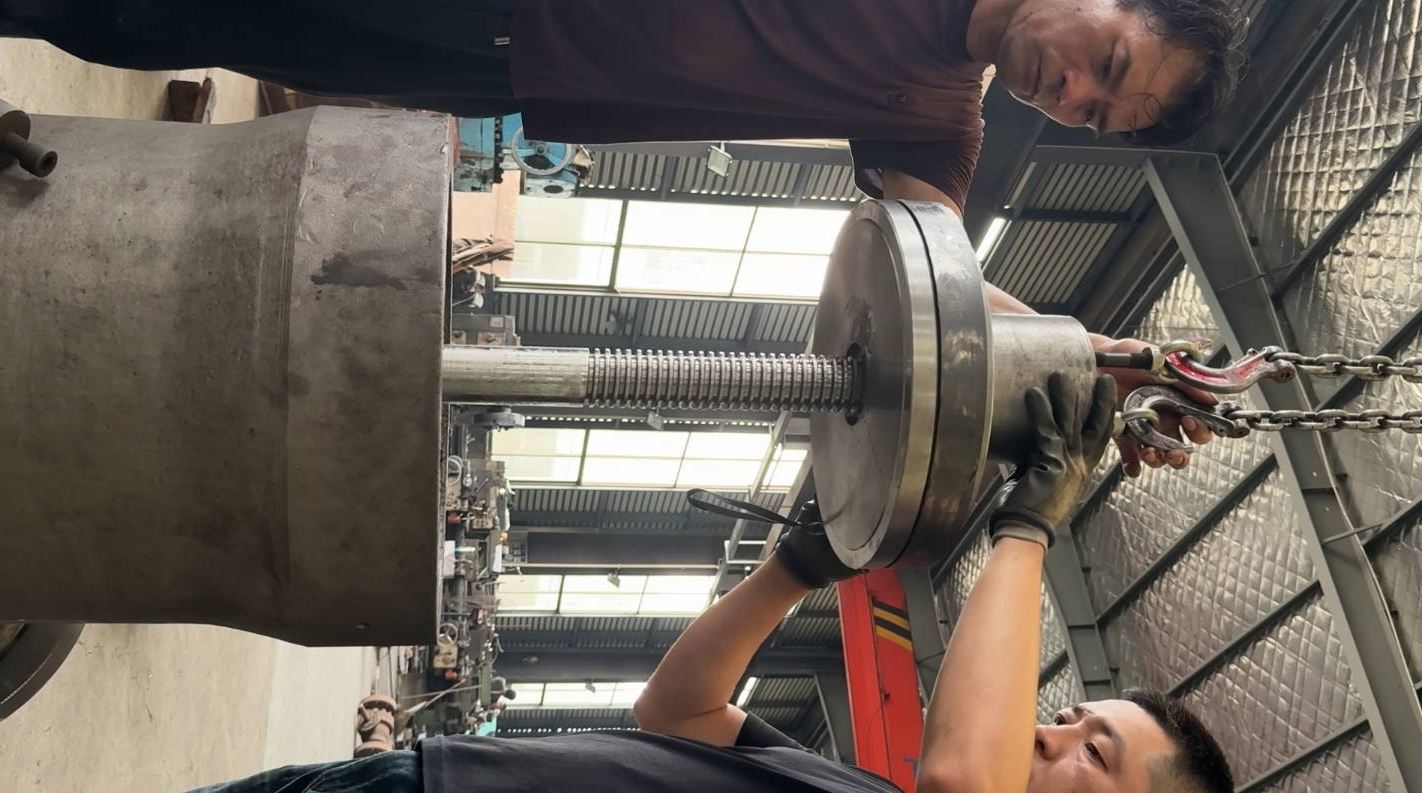 04
Internal Component HandlingHoist-assisted positioning of a large internal component during workshop assembly.
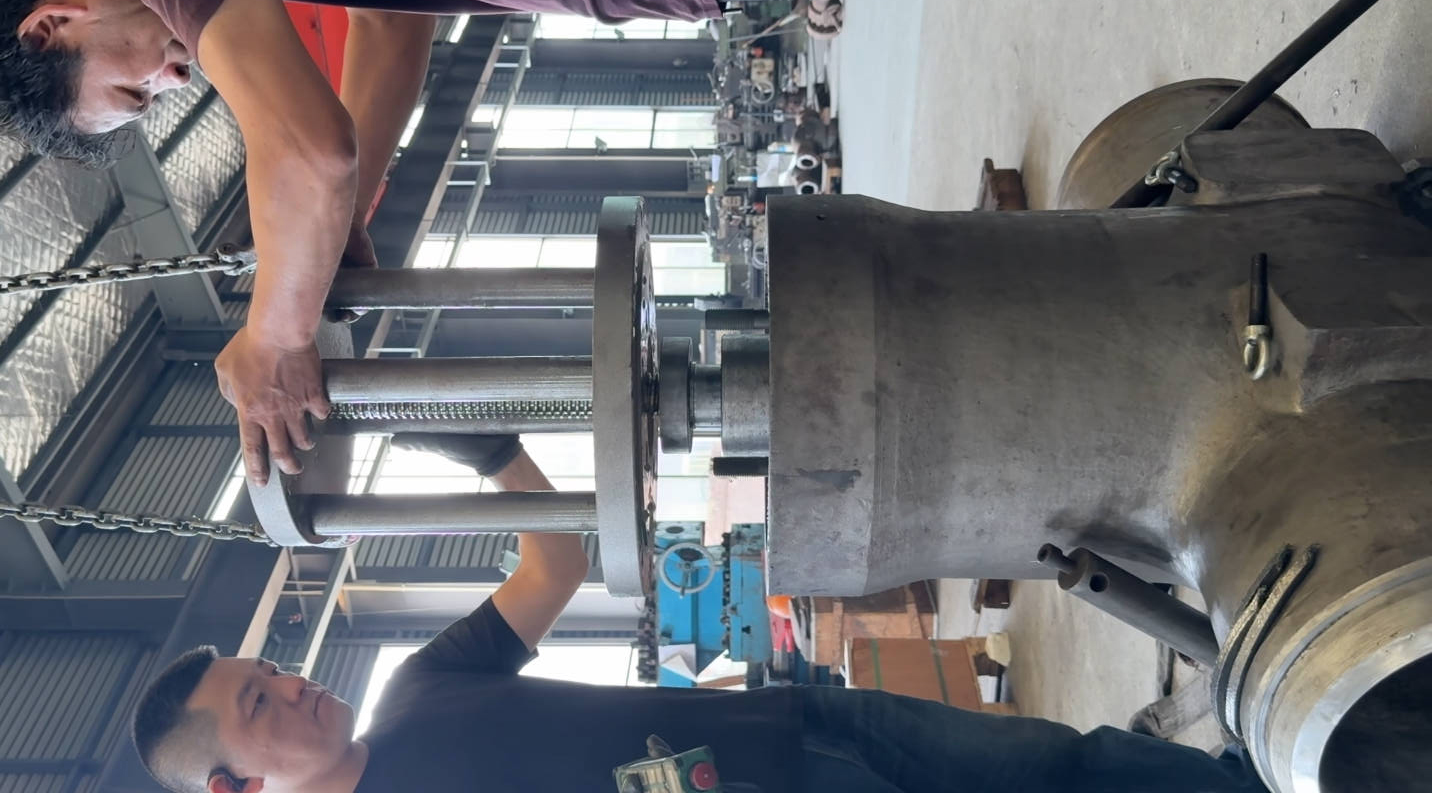 05
Stem and Support AssemblyAlignment of the stem and upper support structure during workshop assembly.
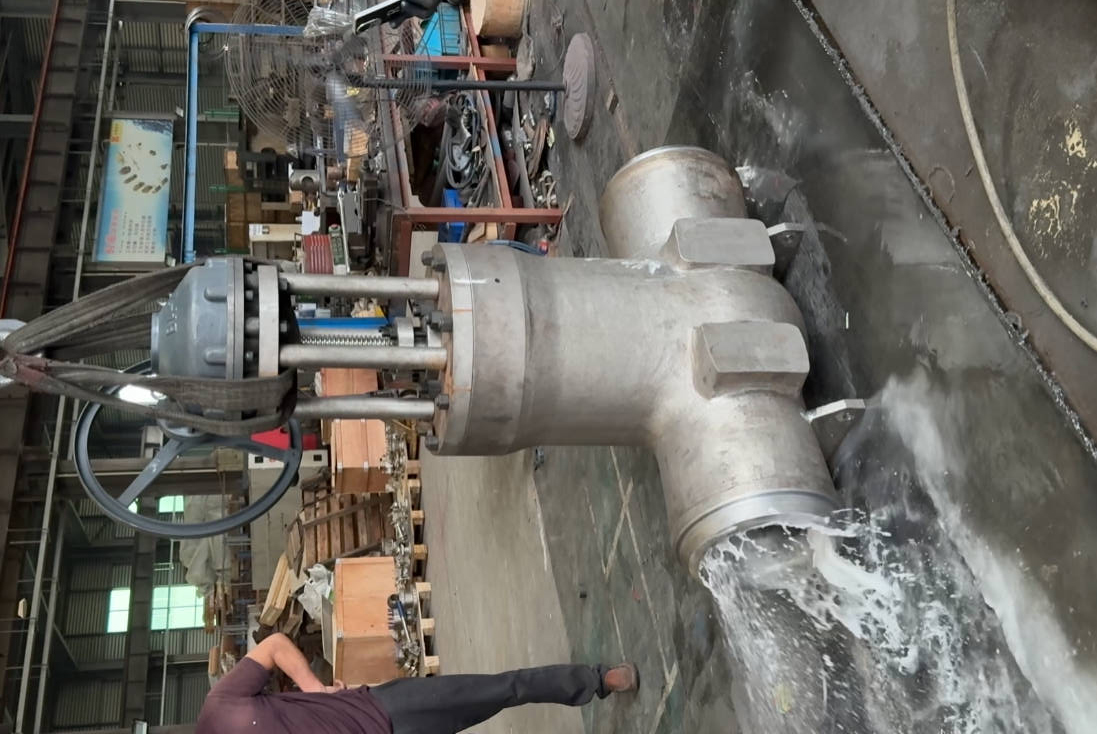 06
Pressure-Test StageVisible workshop stage of the specified API 598 pressure-test procedure; acceptance is documented in the test record.
Manufacturing and Inspection Scope
This case documents visible manufacturing, assembly and pressure-test stages for a DN300 PN100 power station gate valve in 20CrMoV. The specified design basis is NB/T 47044, and pressure testing is specified to API 598.
The approved drawing, purchase specification and inspection and test plan define the final configuration and acceptance criteria. Photographs and video document workshop activity but do not by themselves establish dimensional compliance, material traceability, pressure-test acceptance, leakage performance, temperature limits or suitability for a specific installation.
| Valve Type | Power station gate valve |
|---|---|
| Nominal Size | DN300 |
| Pressure Rating | PN100 |
| Material | 20CrMoV |
| Design Standard | NB/T 47044 |
| Pressure Test Standard | API 598 |
Final configuration, dimensions, end connections, trim, operating method and acceptance requirements remain subject to the approved order documents.
Items Controlled During Manufacturing and Assembly
- Valve body and component identification against the production traveller and material records.
- Machined dimensions, connection interfaces and accessible sealing surfaces against the approved drawing.
- Closure, stem, bonnet and upper-support alignment, together with operating movement during assembly.
- Pressure testing to the approved API 598 procedure, with the test pressure, holding time, medium and acceptance result recorded in the test documentation.
- Marking, coating or preservation, accessories and final assembly status as required by the order.
Documents to Request Before Shipment
Depending on the purchase order, the release package may include the approved drawing, bill of materials, 20CrMoV material certificates, traceability records, dimensional reports, applicable NDE reports, inspection and test plan, API 598 pressure-test procedure and result sheet, marking records, coating or preservation records, and final packing photographs.
Project Release Basis
Project release should reference the approved drawing, bill of materials, material certificates, inspection and test plan, API 598 pressure-test procedure and result sheet, and traceability records.
End connections, face-to-face dimensions, pressure-temperature basis, trim, operating method, leakage acceptance, NDE extent, coating, packing and shipping preservation remain order-specific until confirmed in the purchase order and approved manufacturing documents.
Need a DN300 PN100 power station gate valve?
Send the datasheet or service conditions for a project-specific technical review.